Cutting fluid does three jobs: it removes heat, it lubricates the cutting interface, and it flushes chips away. Different operations need different balances of the three — and in at least one common case, the right answer is no coolant at all.
Flood Coolant
The default in most shops: a generous stream of water-based emulsion over the cutting zone.
Best for: general milling and turning of steel and stainless, drilling, and anything producing lots of chips that need flushing.
Watch out for: concentration. Too weak and you lose lubricity and invite corrosion and bacteria; too strong and you waste money and can irritate skin. Check with a refractometer — 6–10% suits most work. Also make sure the flow actually reaches the cut and is not deflected by the tool or fixture.
High-Pressure Coolant
The same fluid at 30–100 bar instead of 3–5.
Why it matters: at high pressure the jet penetrates the vapour barrier that forms at the cutting edge, and it mechanically breaks chips. In titanium and superalloys it can double tool life. In deep drilling it is what makes single-pass holes possible.
Best for: titanium, superalloys, deep holes, and any operation where chip control limits productivity.
MQL — Minimum Quantity Lubrication
A tiny quantity of oil (typically 10–50 ml/hour) atomised into an air stream.
Best for: aluminium, and general milling where lubrication matters more than cooling. Much cleaner than flood, cheaper to run, and parts come off nearly dry.
Not suitable for: deep holes or heavy roughing that generate more heat than an air stream can carry away.
Dry Machining
No fluid at all — the tool relies on its coating to survive the heat, and the chip carries the heat away.
Best for:
- Cast iron. Traditionally cut dry; the graphite is self-lubricating and coolant creates an abrasive slurry.
- Hard milling above HRC50. This surprises people, but it is important: an edge that is hot by design is thermally shocked every time it exits the cut into cold coolant, causing comb cracks. Compressed air to clear chips gives longer life than flood.
Through-Tool: Where It Really Counts
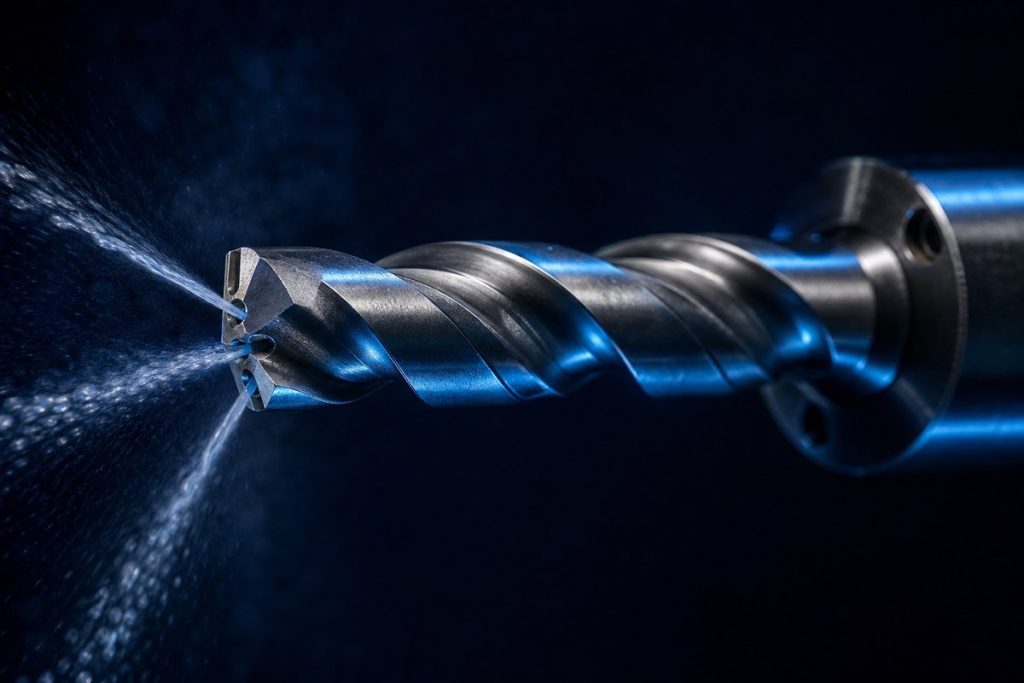
Internal channels deliver fluid directly to the cutting edge instead of relying on it finding its way in from outside.
- Deep drilling — effectively mandatory beyond 5×D.
- Deep pockets — where external flow cannot reach the bottom.
- Parting off — a blade with internal coolant transforms this operation, particularly in stainless.
- Reaming and boring — flushes chips ahead of the tool so they cannot score the finished bore.
Choosing Quickly
| Operation | Recommended |
|---|---|
| General steel milling | Flood |
| Aluminium milling | MQL or flood |
| Cast iron | Dry or air |
| Hardened steel milling | Air / MQL (avoid flood) |
| Stainless turning | Flood, high pressure if available |
| Titanium & superalloys | High-pressure through-tool |
| Deep hole drilling | Through-tool, 40–70 bar |
| Parting off | Through-blade coolant |
Aim Before You Add More
The most common coolant problem is not quantity but direction. A nozzle pointing at the general area of the tool does far less than a nozzle pointing at the cutting edge. Before increasing flow, spend two minutes aiming what you already have — it is usually the cheapest tool-life improvement available.
Many of our drills and grooving blades are available with internal coolant channels. Tell us your setup and we will advise on the right configuration.
Talk to Our Engineers
MSU Tools manufactures the full range of solid carbide and indexable tooling discussed here. Tell us your material, machine and application and we will recommend the optimal tool, grade and starting parameters — or design a custom tool to your drawing. Send us your requirement for a reply within one business day.
Questions about this topic?
Our engineers are happy to advise on tools, grades and cutting parameters.